Why Conveyor Layout Affects the Whole Bottling Line
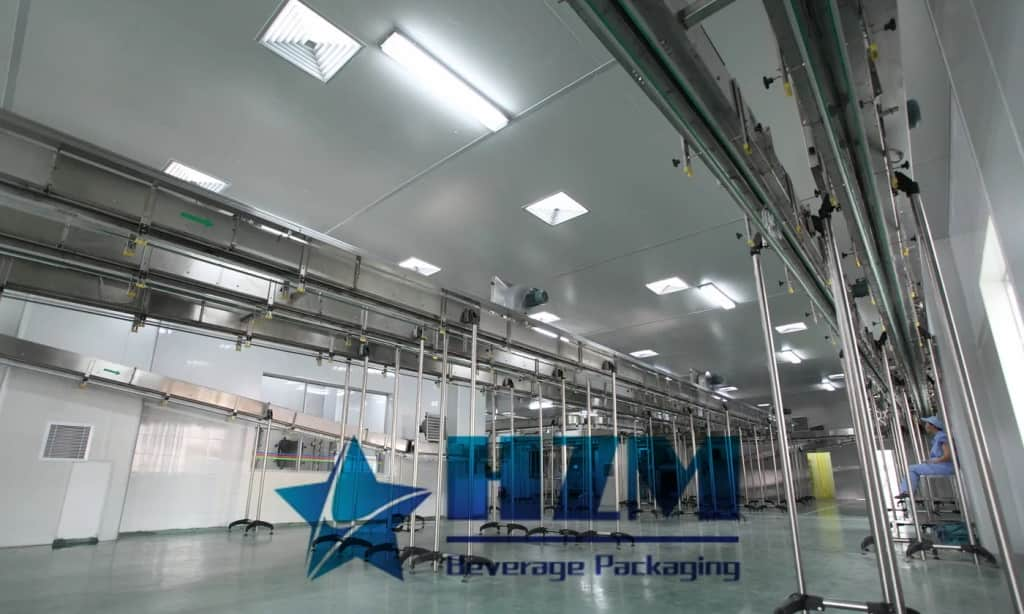
Conveyors connect machines with different operating cycles and interruptions. Their task includes stable transfers and controlled accumulation, not just moving bottles at a stated belt speed.
Size the useful buffer
Count how many containers can accumulate safely between the relevant machines. Relate that quantity to the upstream output and expected stop duration. An accumulation section cannot absorb an indefinitely blocked downstream machine.
Observe every handover
Inspect gaps, height changes, guides and sensor positions with the least stable approved bottle. Test blockage and controlled restart. Record where bottles first tip or become scuffed before changing speeds throughout the line.
Express buffer capacity in minutes
For illustration, 600 usable bottle positions represent two minutes of incoming production at 300 bottles per minute, if the buffer starts empty and downstream output is zero. Partial occupancy reduces that time. This calculation helps identify whether the buffer can cover a typical short stop; it does not prove that the bottles tolerate the resulting contact pressure.
Need help planning your packaging line?
Share your product, bottle and capacity requirements for a practical equipment recommendation.
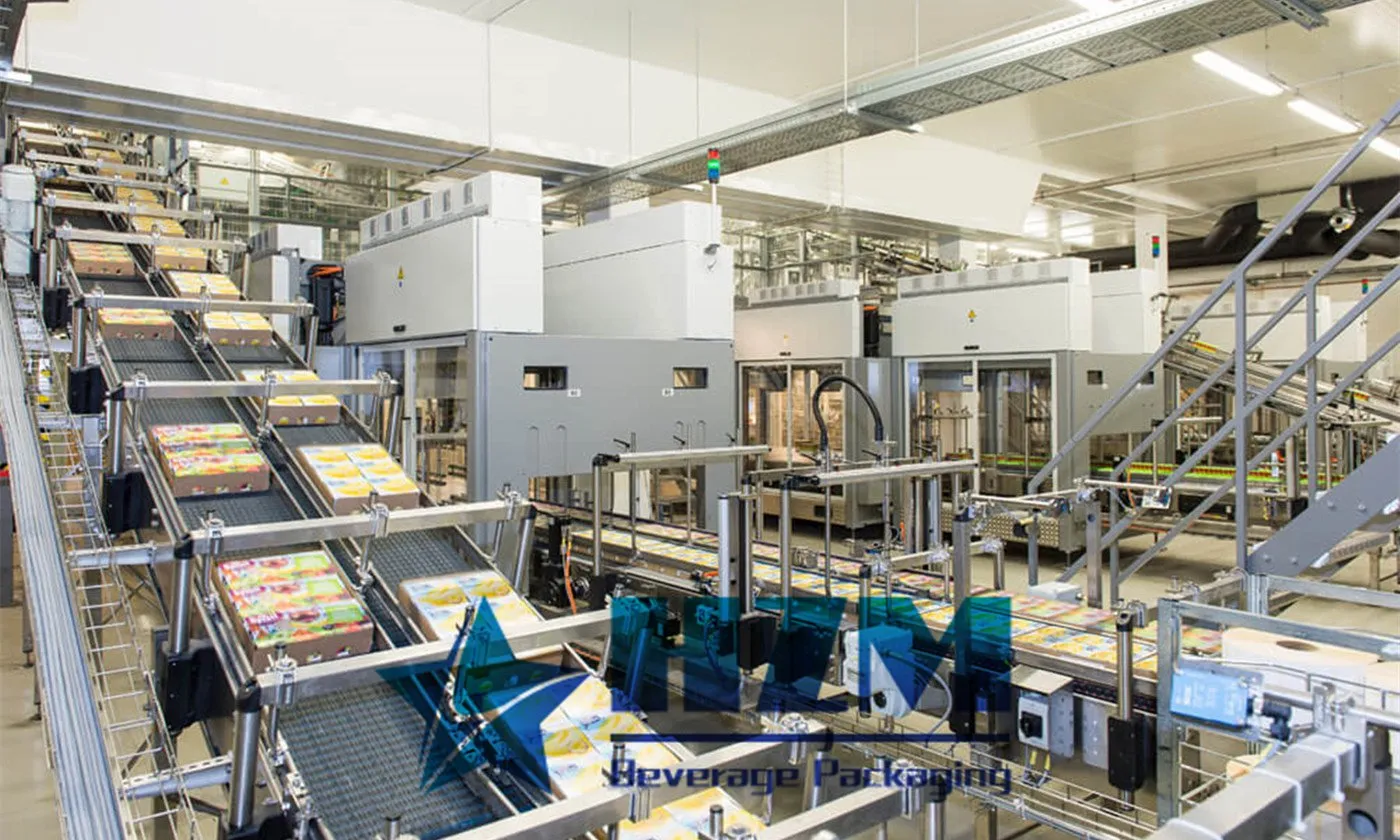
Packs Conveyor
The packs conveyor moves finished packs, cartons and other packaged products between packing and handling stations.
Learn more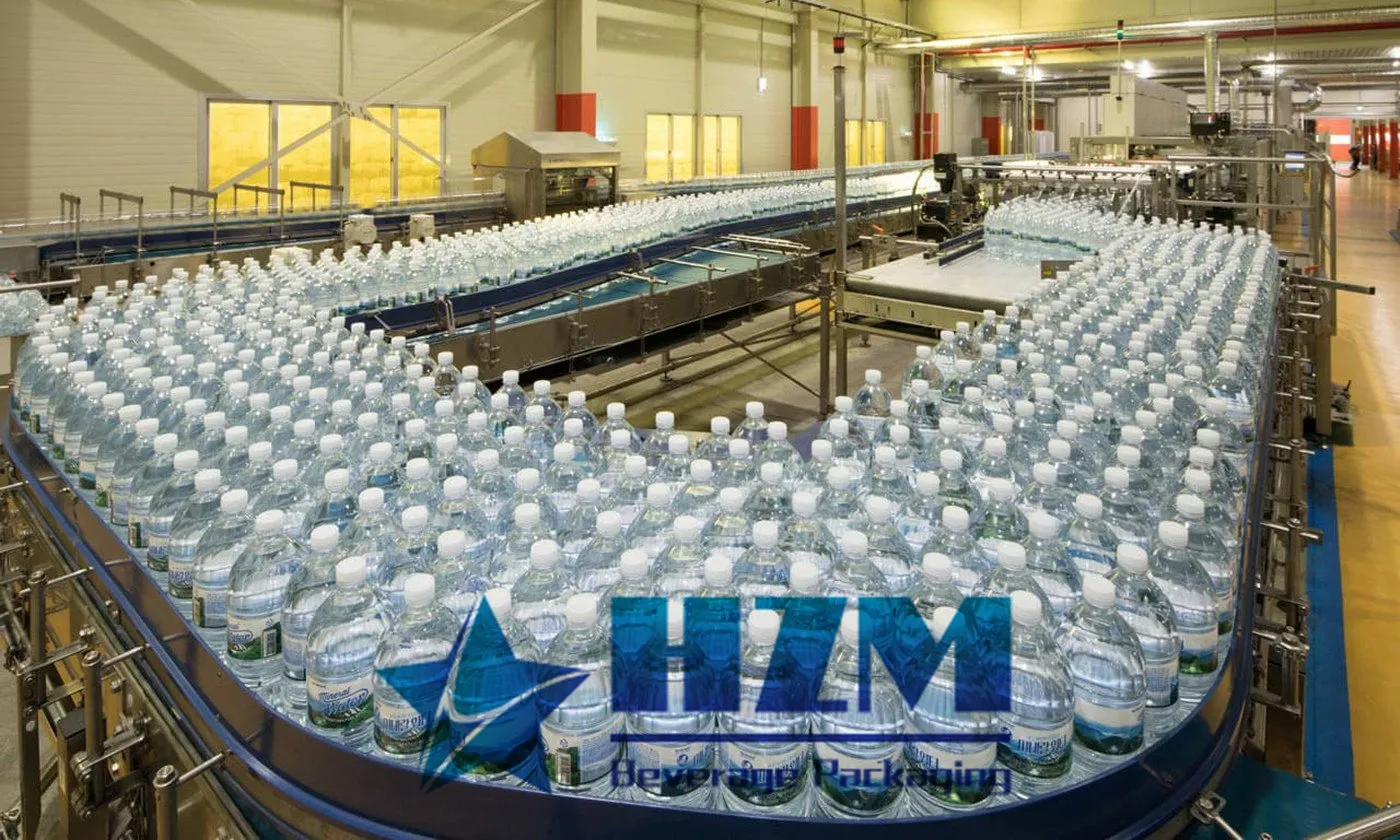
Bottle Conveyor
The bottle conveyor transfers containers between filling, labelling and packing machines.
Learn more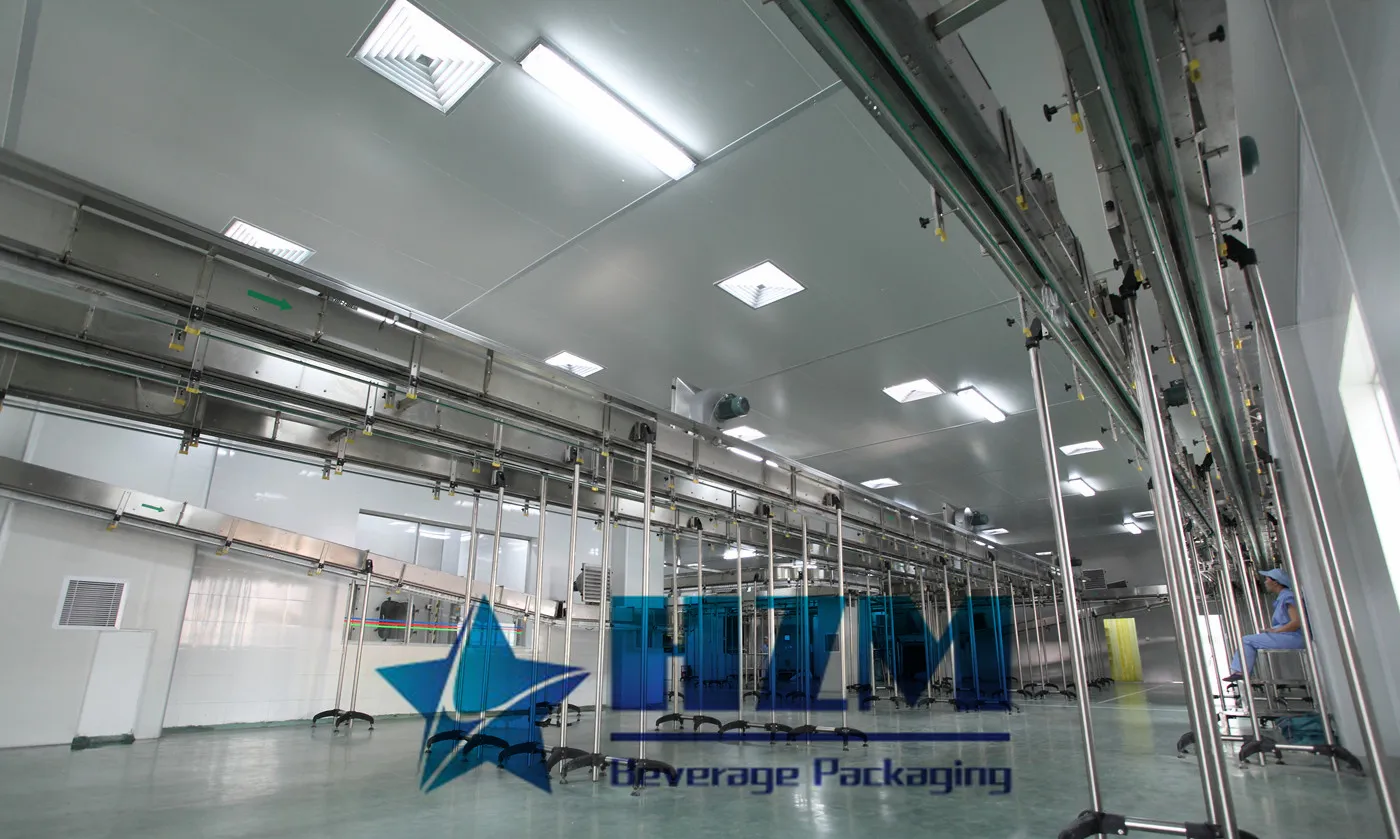
Bottle Air Conveyor
The bottle air conveyor transfers empty PET bottles from the blowing machine to the filler.
Learn more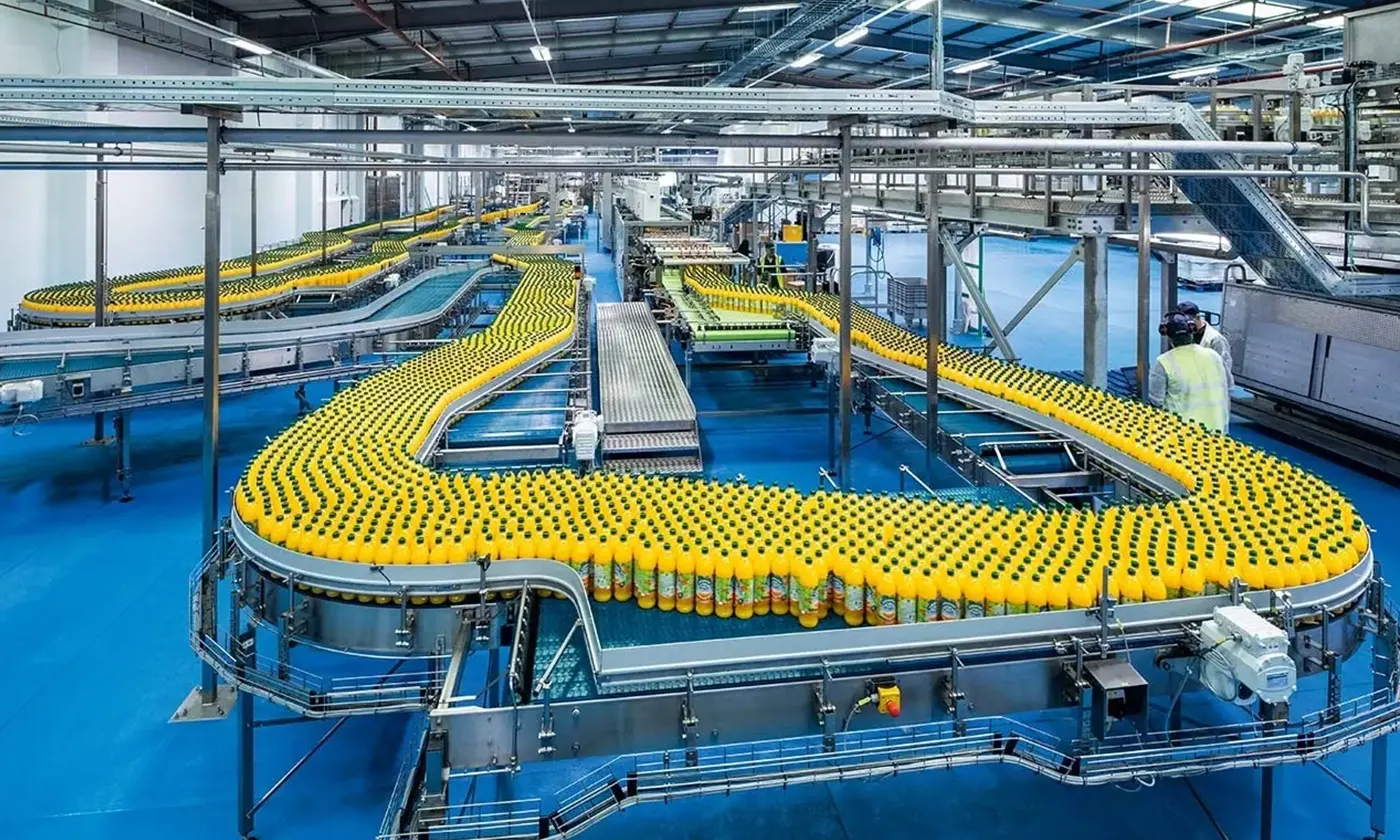
Bottle Water & Beverage Conveyor System
The bottled-water and beverage conveyor system connects container supply, filling and packaging.
Learn more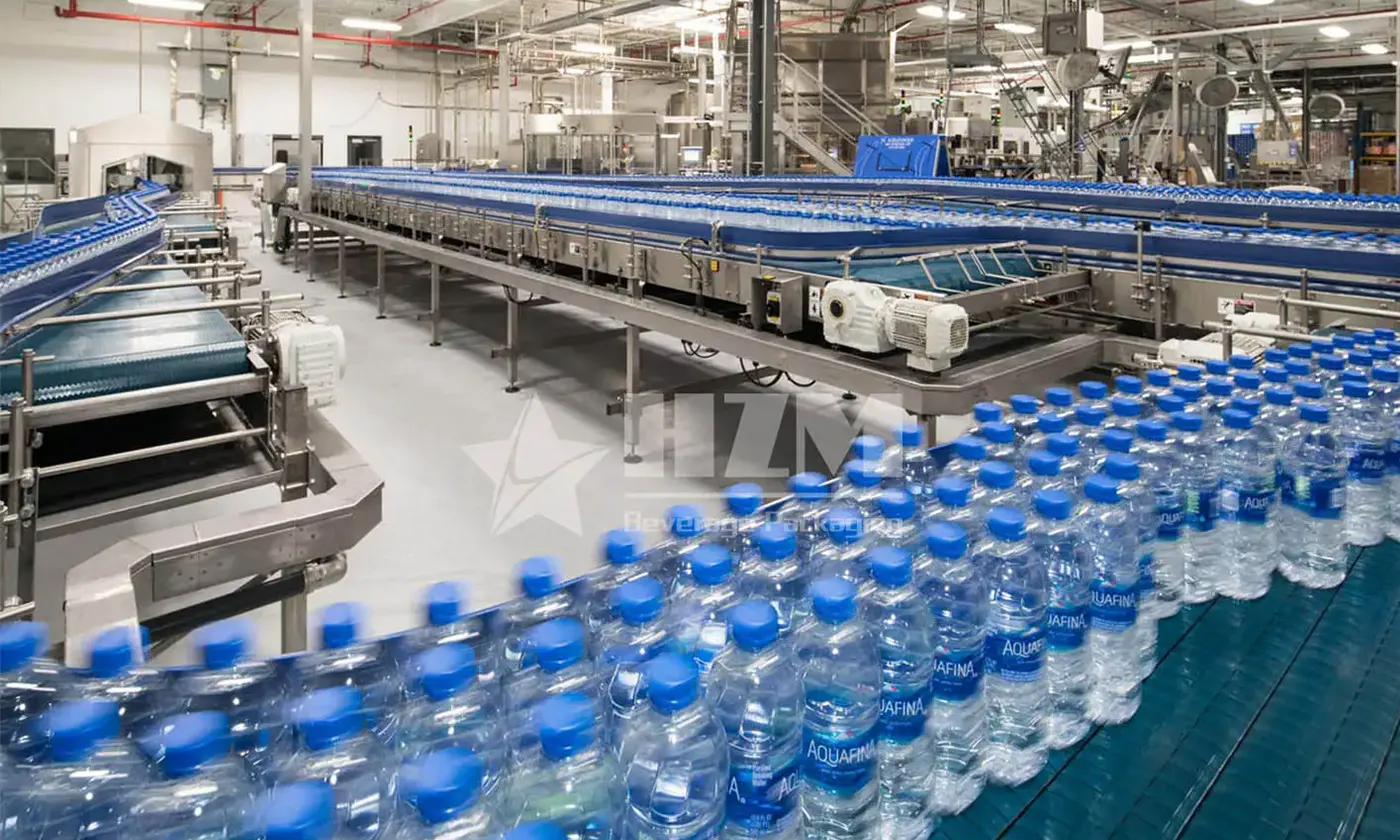
Conveyor Belt For Bottle Water Production Line
This conveyor belt system moves bottles through a bottled-water production line, from empty-bottle feeding to filled-bottle labelling and packing.
Learn more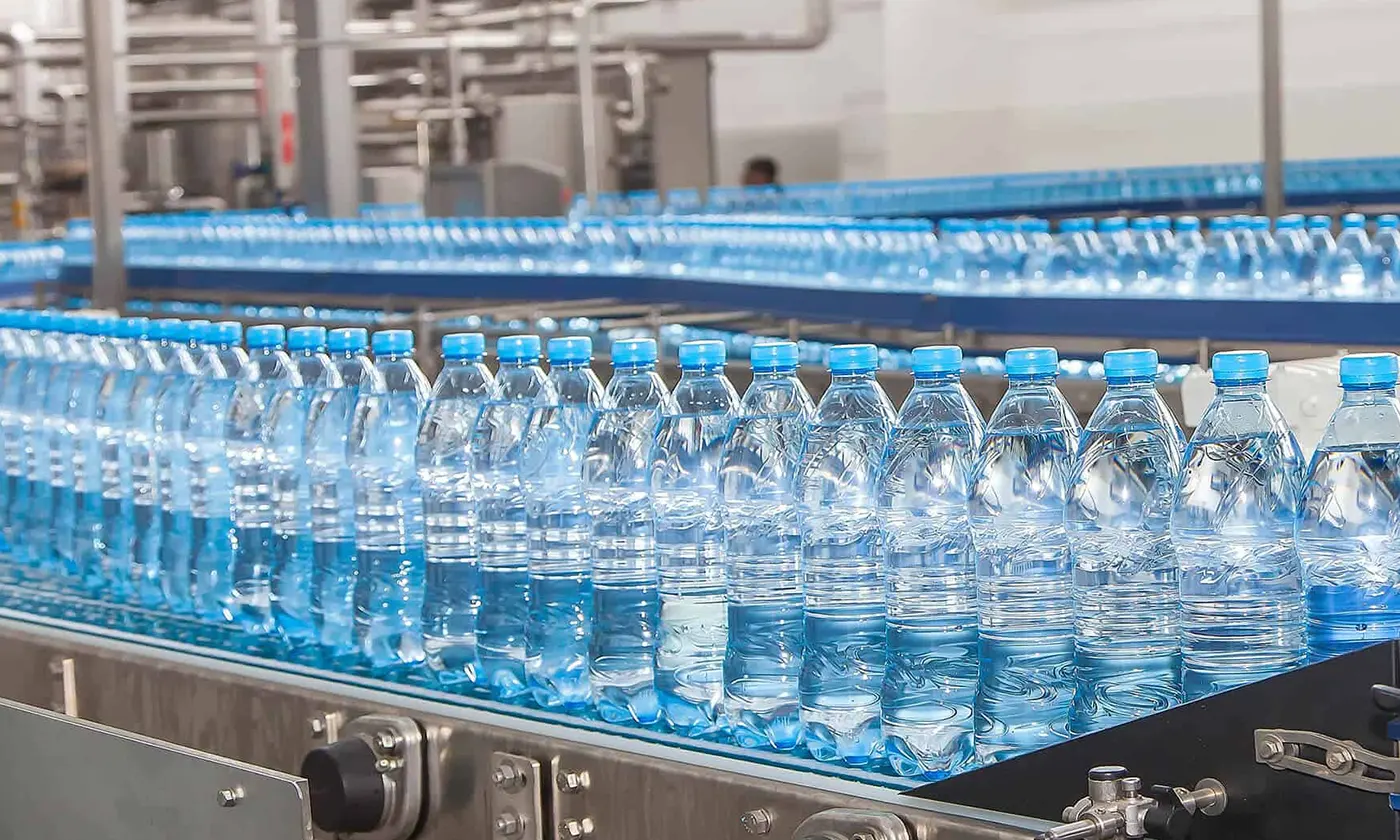
Conveyor Belt System For PET Bottle And GLASS Bottle
The conveyor system transfers PET and glass bottles between production machines.
Learn more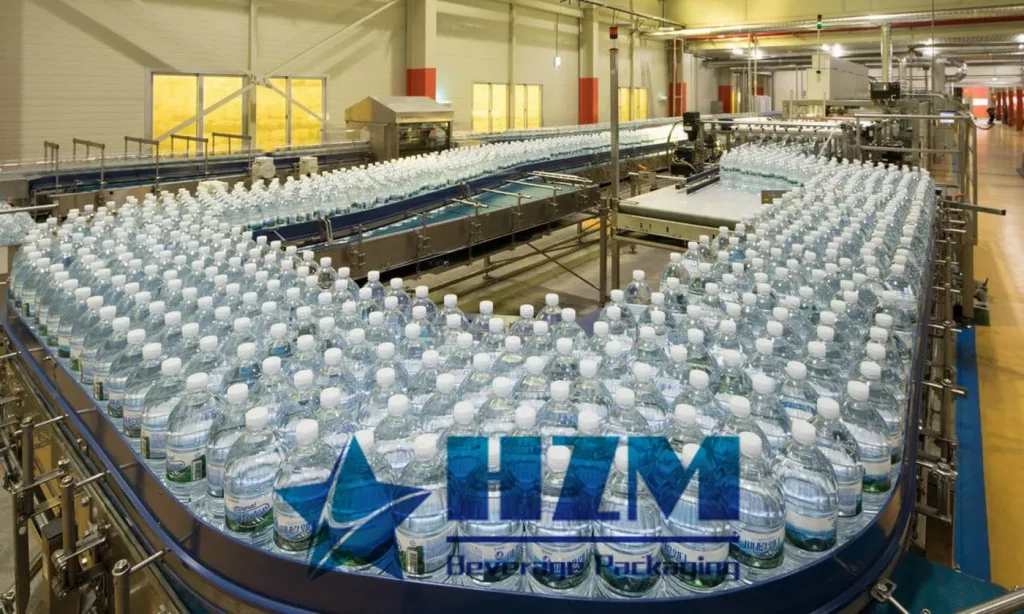
Your Reliable Conveyor Machine Manufacturer
In modern industrial production, Conveyor Machines are indispensable for efficient material transportation and automated production. When seeking a trusted manufacturer, HZM Machinery stands out as a reliable partner.
Learn moreSpecifying Bottle and Pack Conveyors at Machine Interfaces
A conveyor quotation should show how each container moves between machines, where it can accumulate and what happens when the next machine stops.
Learn more
Top 10 Conveyor Machine Brands in the Industry, Including HZM Conveyor Machine
Conveyor machines play a vital role in modern industrial production, widely used in logistics, manufacturing, packaging, and other fields. Among the numerous conveyor machine brands
Learn moreAir conveyor systems
The air conveyor, also known as a pneumatic conveyor, serves the purpose of efficiently transporting empty bottles between machines within a filling line. It also acts as a buffer, allowing for automatic operation of the entire line. Primarily, it is employed to transfer empty PET bottles from the blowing machine to the filling machine, also known as the filler.
Learn more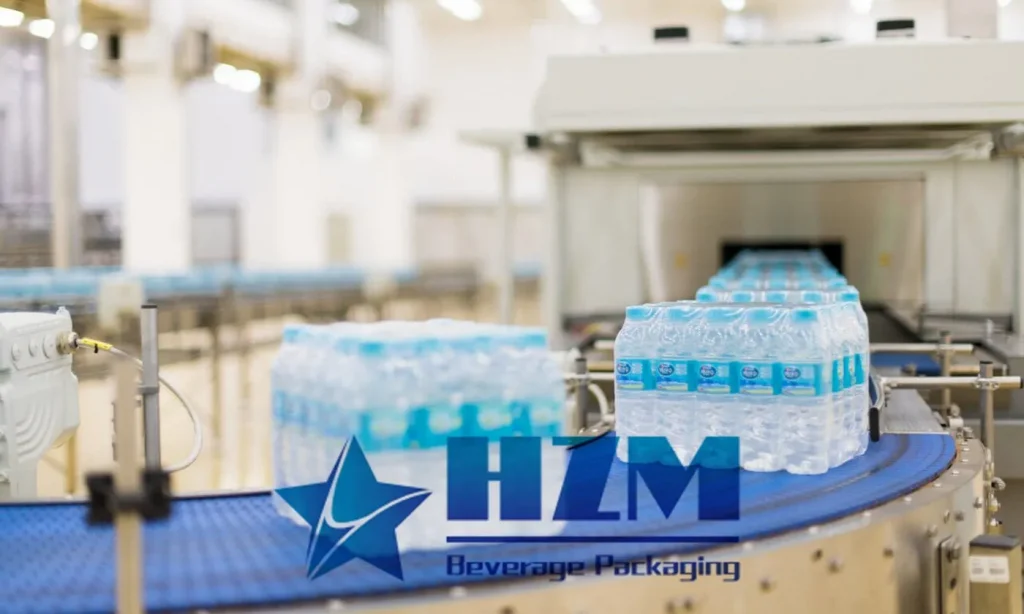
Finding the First Unstable Point on a Bottle Conveyor
A pile-up is often the result of an earlier catch, failed transfer or missed sensor signal.
Learn more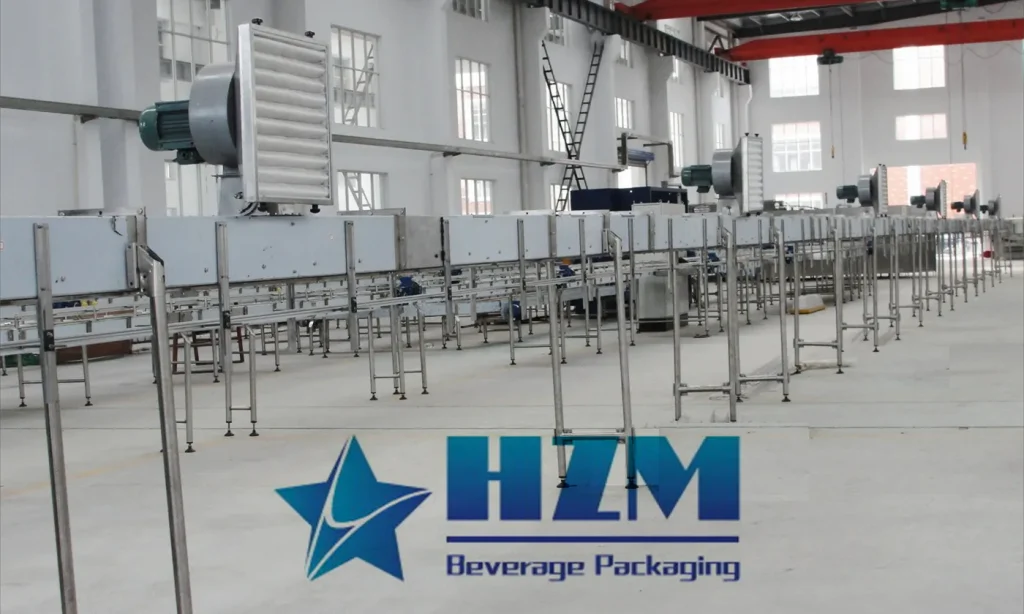
What Changes the Price of a Bottle Air Conveyor?
An air-conveyor quotation depends on route geometry, neck-handling requirements, supports, switches and machine connections.
Learn more