Matching a Bottle Conveyor to Empty and Filled Containers
Empty PET bottles and filled bottles have different handling behaviour. Neck-supported air conveying is a different application from a belt or chain supporting a filled container’s base. Select the conveyor route for the actual container state.
Inspect transfers under load
Check guide contact, gaps, level changes and accumulation with production bottles. Filled-container weight can expose instability that an empty-bottle test misses. Include the least stable approved format.
Coordinate stop signals
Define how each section responds to a blocked discharge or missing infeed. Test restart without manual pushing. Record tipping and scuffing at their first location so a local defect can be corrected without changing the entire conveyor’s speed.
Need help planning your packaging line?
Share your product, bottle and capacity requirements for a practical equipment recommendation.
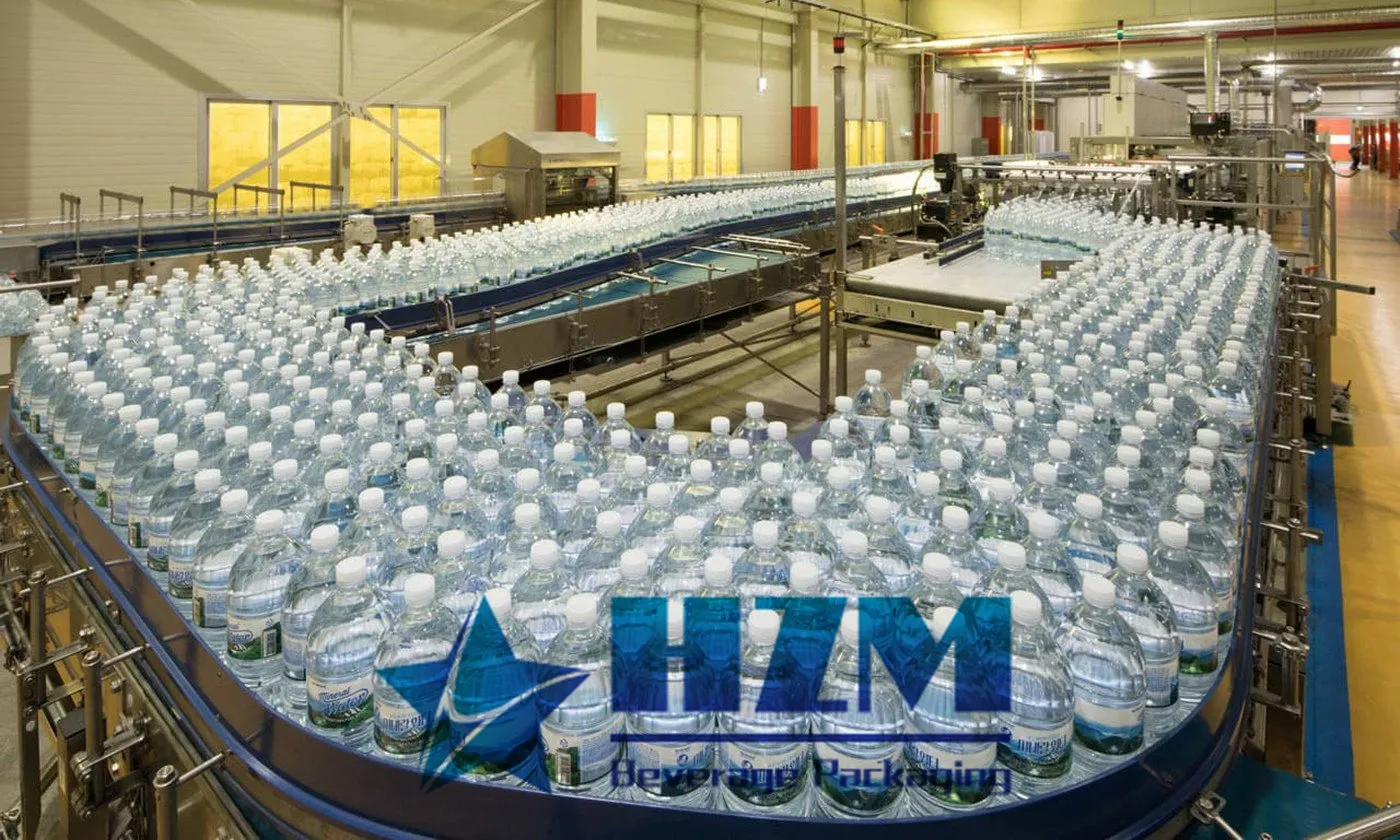
Bottle Conveyor
The bottle conveyor transfers containers between filling, labelling and packing machines.
Learn more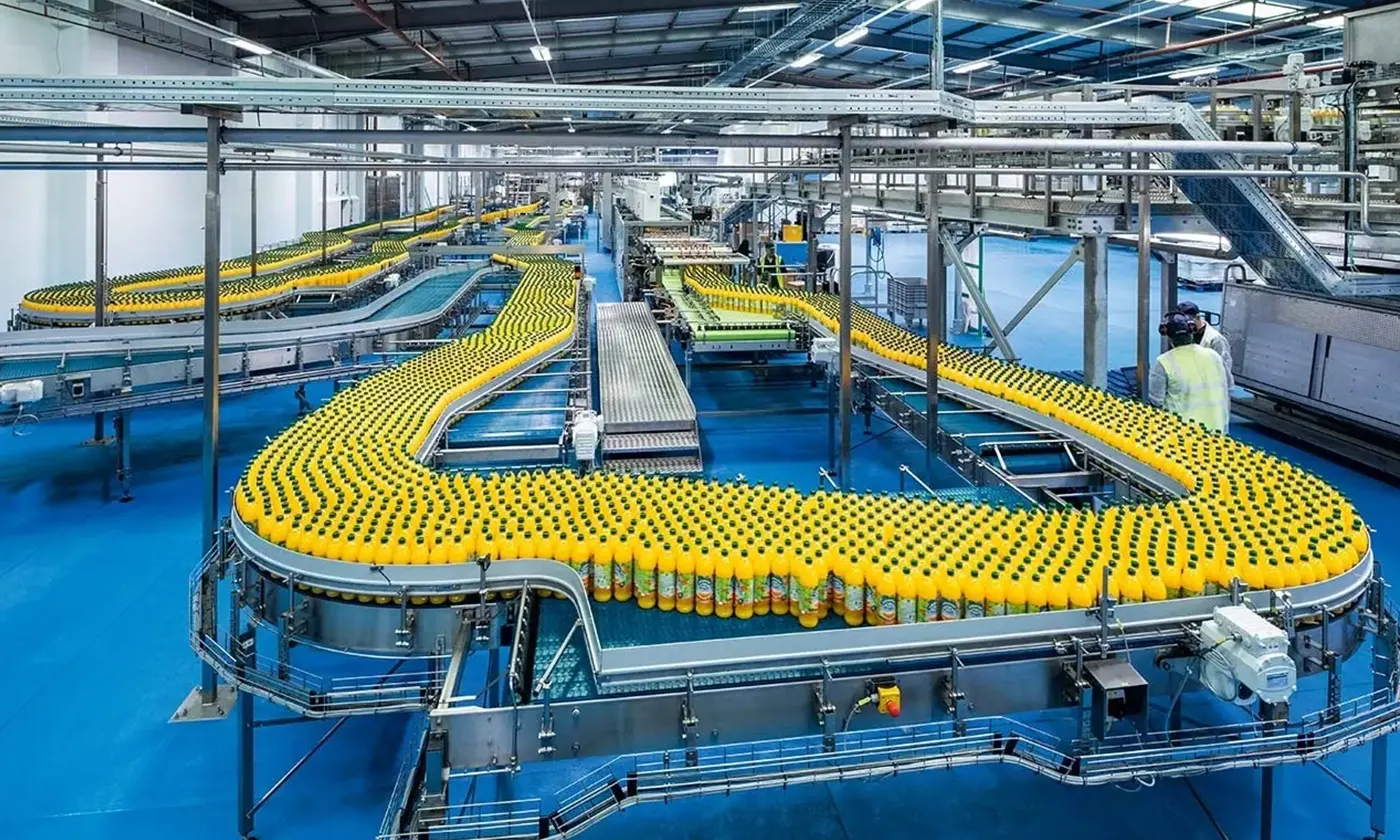
Bottle Water & Beverage Conveyor System
The bottled-water and beverage conveyor system connects container supply, filling and packaging.
Learn more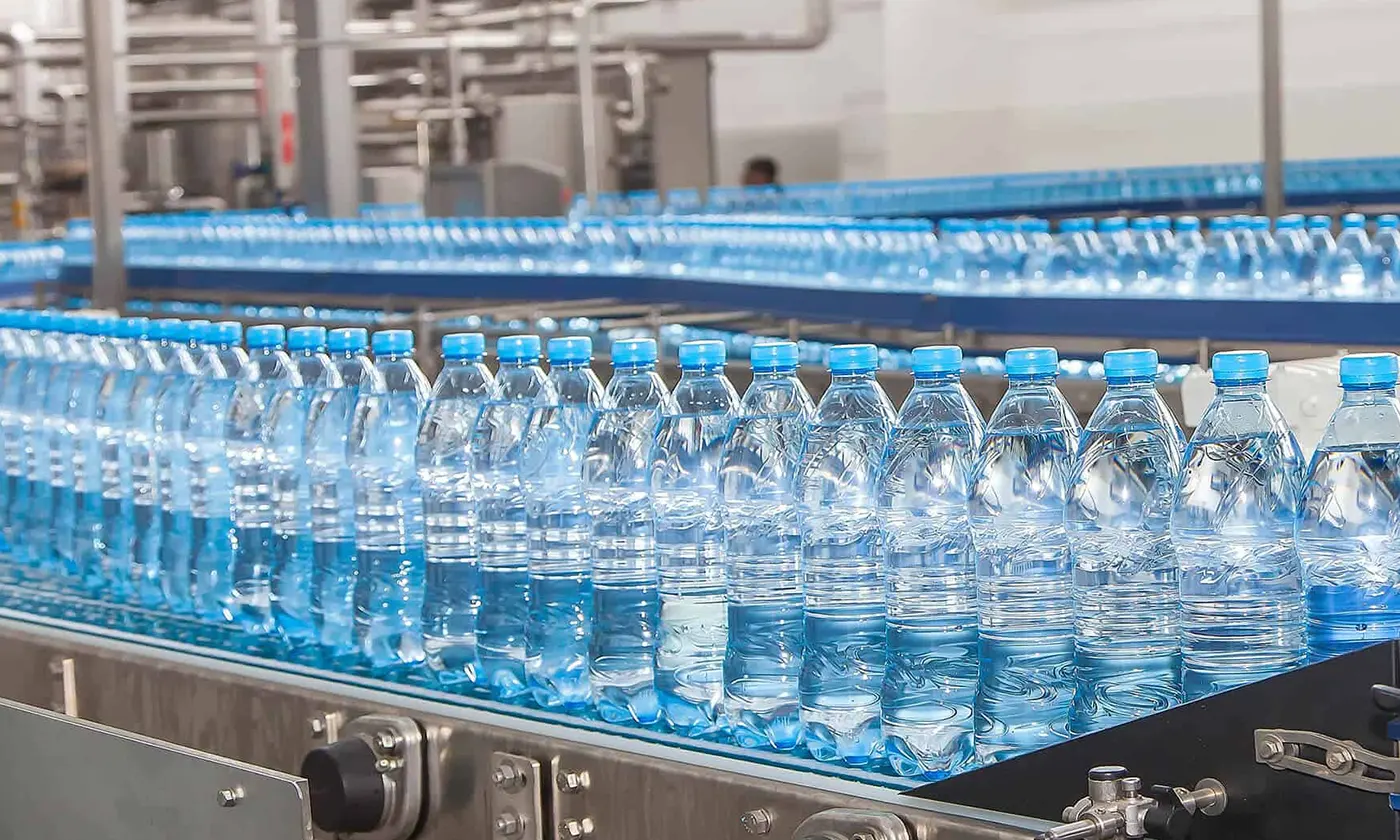
Conveyor Belt System For PET Bottle And GLASS Bottle
The conveyor system transfers PET and glass bottles between production machines.
Learn more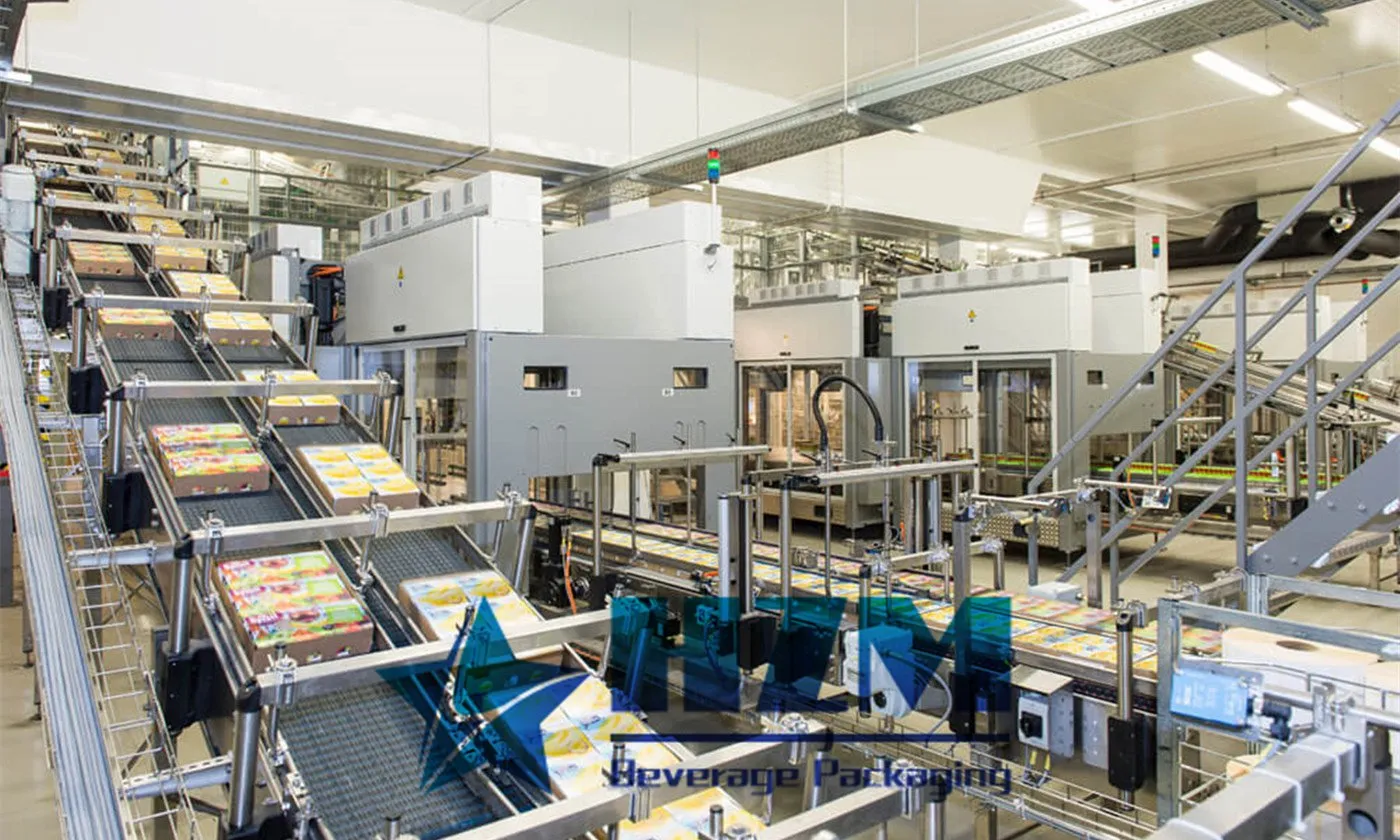
Packs Conveyor
The packs conveyor moves finished packs, cartons and other packaged products between packing and handling stations.
Learn more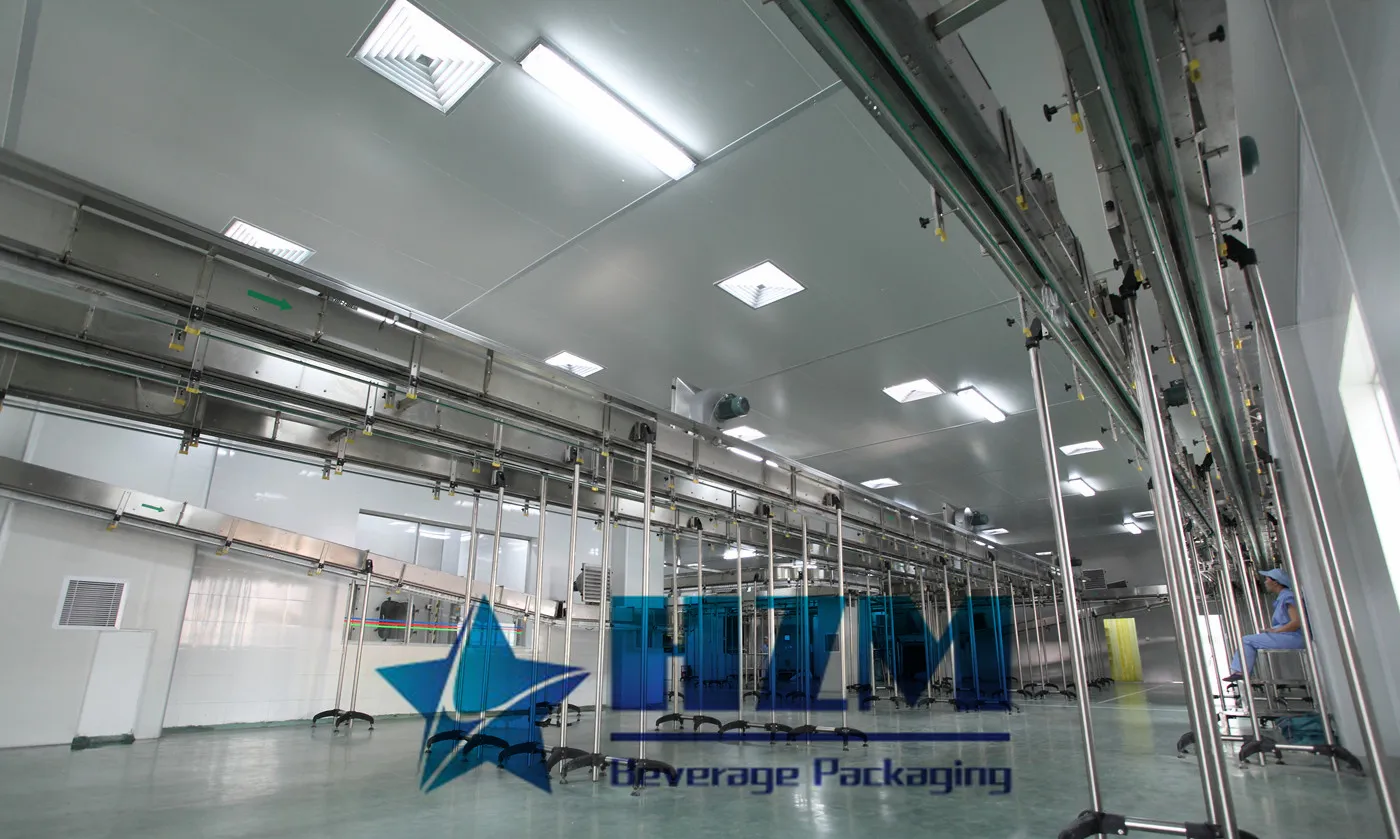
Bottle Air Conveyor
The bottle air conveyor transfers empty PET bottles from the blowing machine to the filler.
Learn more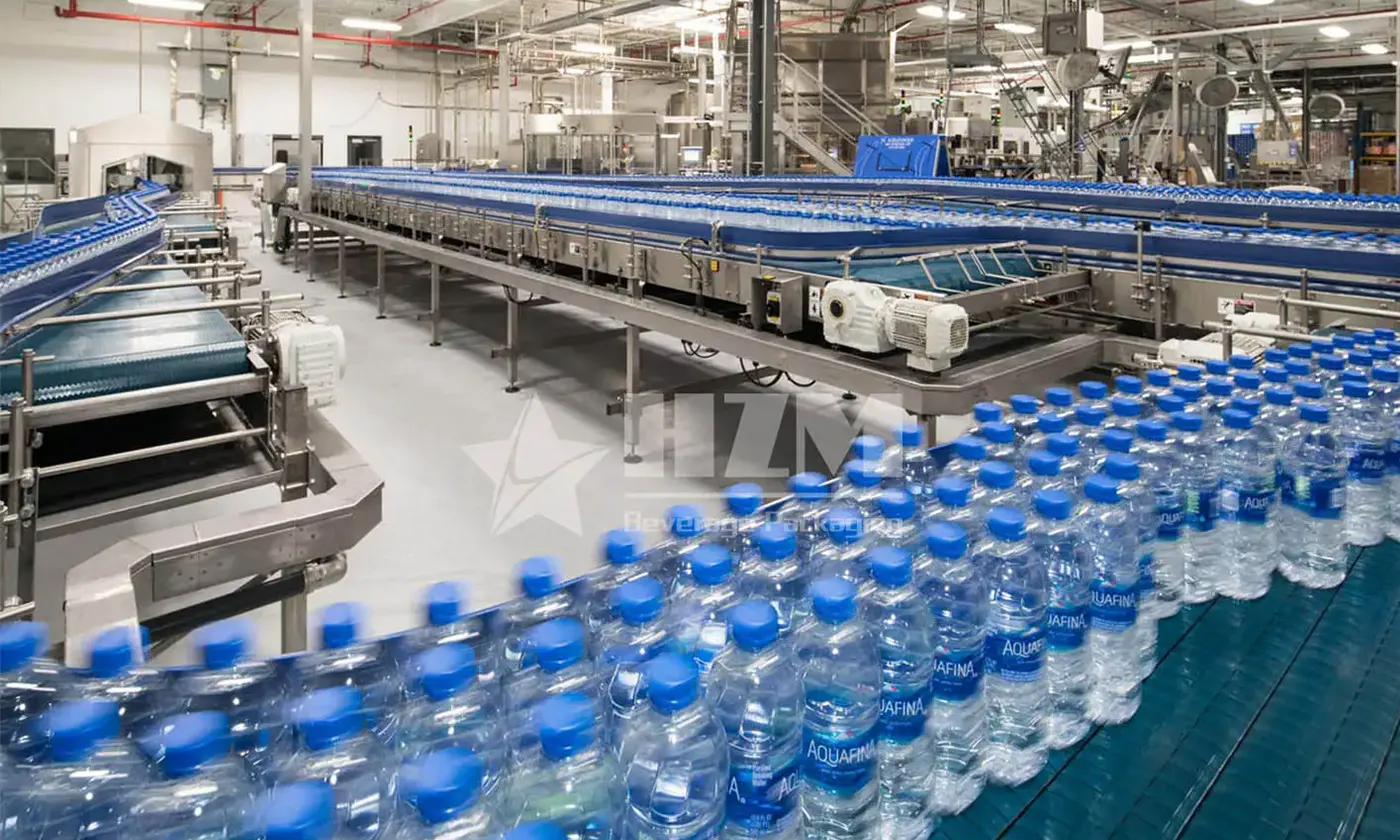
Conveyor Belt For Bottle Water Production Line
This conveyor belt system moves bottles through a bottled-water production line, from empty-bottle feeding to filled-bottle labelling and packing.
Learn more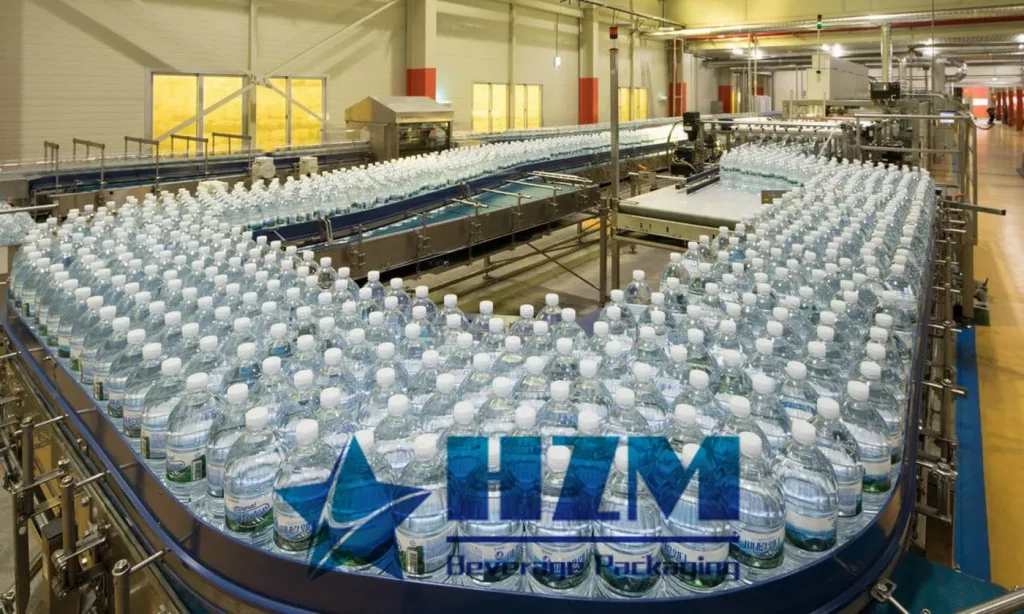
Your Reliable Conveyor Machine Manufacturer
In modern industrial production, Conveyor Machines are indispensable for efficient material transportation and automated production. When seeking a trusted manufacturer, HZM Machinery stands out as a reliable partner.
Learn morePET Bottles Fall Over on the Conveyor
Evaluate bottle stability, fill level, base shape, guide height and clearance, conveyor speed transitions, air movement and accumulation. Lightweight bottles need controlled support without being squeezed. Follow this practical fault-isolation, repair and prevention guide for bottling-line operators and maintenance teams.
Learn moreAir conveyor systems
The air conveyor, also known as a pneumatic conveyor, serves the purpose of efficiently transporting empty bottles between machines within a filling line. It also acts as a buffer, allowing for automatic operation of the entire line. Primarily, it is employed to transfer empty PET bottles from the blowing machine to the filling machine, also known as the filler.
Learn moreBottle Sensors Trigger False Stops on a Beverage Conveyor
Preserve the input state, then check sensor cleanliness and alignment, transparent-bottle suitability, reflector condition, vibration, background reflection, mutual interference,.
Learn moreBottle Conveyor Jams at the Same Location Every Shift
Mark the first contact point and inspect guide transitions, chain condition, dead plates, speed change, bottle dimensions, lubrication and upstream accumulation. The pile-up often occurs downstream of the actual interference. Follow this practical fault-isolation, repair and prevention guide for bottling-line operators and maintenance teams.
Learn moreConveyor VFD Trips on Overcurrent: Electrical or Mechanical?
Record the exact fault and operating state before reset. With qualified electrical personnel, separate mechanical binding and acceleration load from motor, cable, parameter, supply and drive faults. Follow this practical fault-isolation, repair and prevention guide for bottling-line operators and maintenance teams.
Learn more